How To Work A Laser Cutter For Metal Tubes
Placing a sheet on a cutting table and clamping a long tube in a chuck involve different operating conditions. Tubes rotate, and long stock requires support. Bowing, cross-section variation, or eccentric clamping can change the relationship between the cutting head and the actual surface.
To understand how to work a laser cutter, consider a metal tube cutting job: which workpiece the program describes, how the tube stays stable, and whether the finished part meets its requirements. This discussion concerns CNC laser tube cutting machines. Their clamping arrangements should not be transferred to sheet cutting machines or other laser equipment.
Match the program to the actual tube
The CNC system converts part geometry, process settings, and motion requirements into axis commands, coordinating tube feeding, rotation, the cutting head, and auxiliary equipment. CAD/CAM software handles tasks such as toolpath generation, nesting, and process parameter retrieval, with available functions depending on the actual configuration. Identical part shapes do not mean that tubes of different materials, wall thicknesses, or cross-sections can share the same process settings.
Automatic parameter retrieval requires matching material, wall thickness, gas, nozzle, and program information. Incorrect data can still produce defective parts. Sheet cutting parameters cannot directly establish tube wall thickness capability or processing cycle times: tube cutting also involves rotation, focus on curved surfaces, clamping, and the opposite wall.
Cutting concentrates laser energy locally, while assist gas removes molten material and reaction products from the kerf. Power, speed, focus, nozzle condition, and gas all affect the result. Increasing power alone does not establish that a given wall thickness can be cut through consistently or that the edge quality will be acceptable.
Account for rotation and support after clamping
Non-contact cutting still requires a stable workpiece. Sagging and movement during rotation affect hole positions, contours, and focus distance. Support conditions must match the tube's length, weight, and cross-sectional stiffness. Outside diameter, roundness, straightness, and weld reinforcement can also cause the actual surface to differ from the theoretical surface in the program.
Thin-walled tubes are particularly sensitive to clamping. Excessive force can flatten them; insufficient force can allow slipping or vibration. If clamping marks or crushing occur, chuck clamping pressure can be reduced while ensuring that the tube does not slip during rotation. Polyurethane or nylon soft jaws can distribute contact stress on thin-walled tubes with demanding surface requirements. They still require appropriate pressure adjustment; changing the jaws does not remove the need to address the clamping condition.
Before startup, cutting head checks include the nozzle, ceramic ring, relevant connections, and fasteners. Contamination on the protective window affects the optical path and cutting stability. A window with burn spots or black marks should be taken out of service and replaced. Abnormal height following, head collisions with the tube, or failed piercing also call for checking the nozzle, beam centering, capacitive sensing, and head connections. These problems cannot all be attributed to the program.
What to examine in a trial cut
After changing any parameter, perform a small trial cut and examine the edge, dross, dimensions, and equipment condition. Assess dimensions and contours separately from burrs, dross, and edge oxidation. Cutting through is only one criterion, and machine axis positioning figures cannot replace measurements of the actual part.
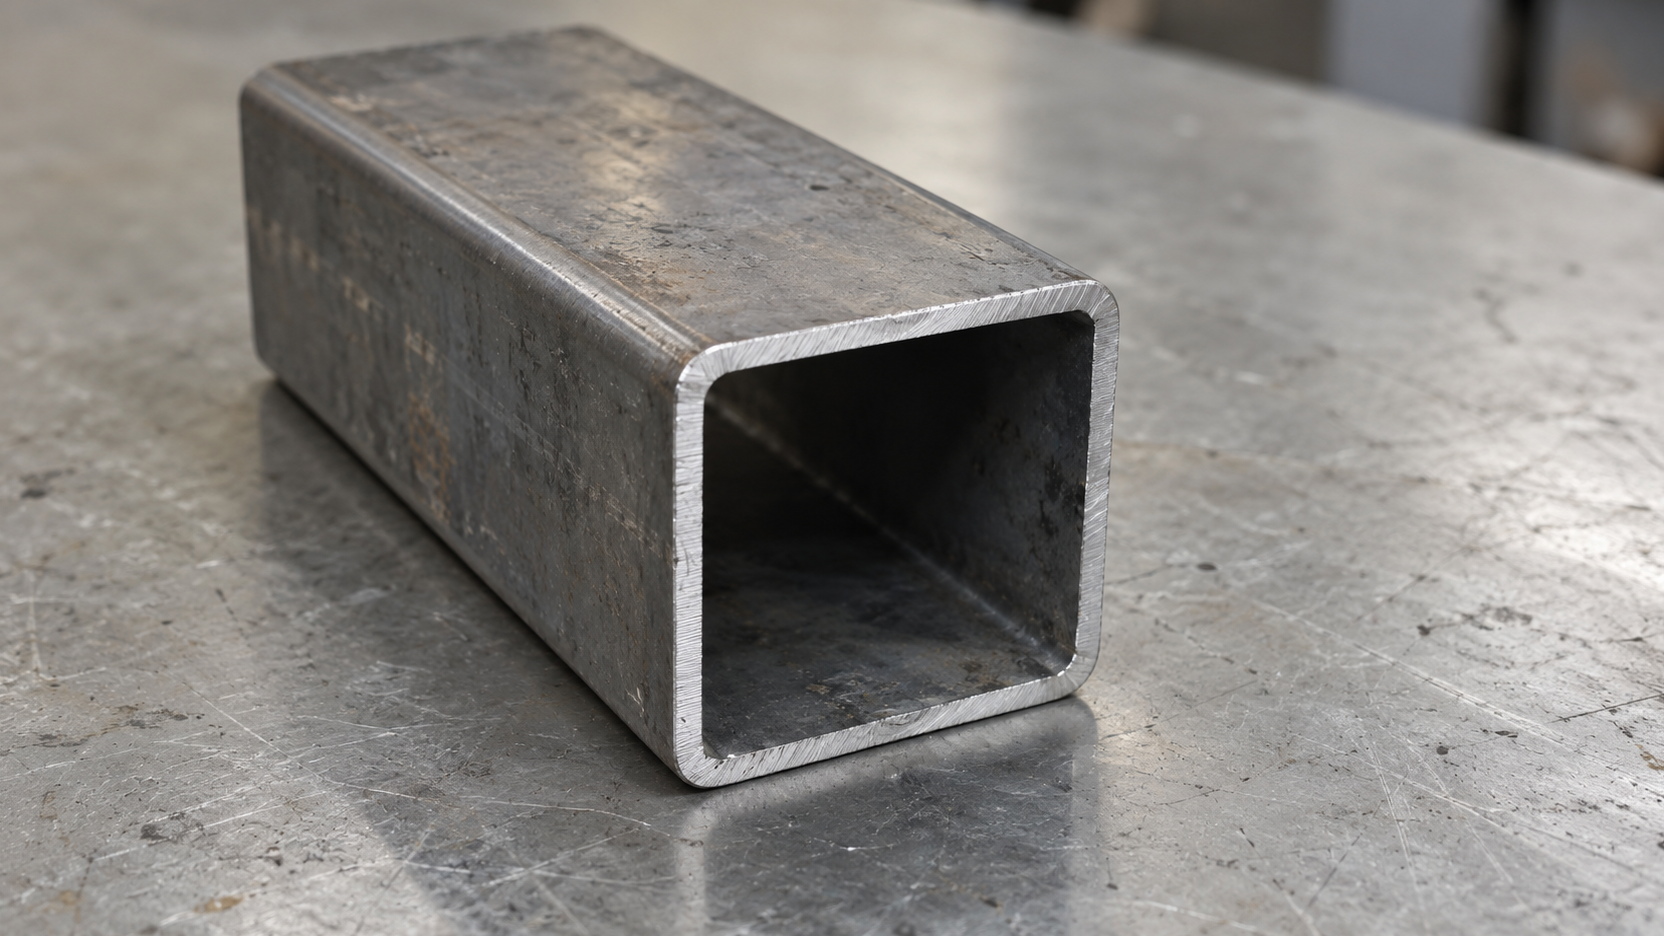
For dross beneath a thick-walled tube or incomplete penetration, the checks include power, speed, focus, piercing mode, nozzle, and assist gas. Excessive speed may prevent full penetration, while insufficient speed may cause overburning or the kerf to fuse back together. Simply reducing speed whenever dross appears does not address these different causes.
Blackening on the opposite wall of a thin-walled tube calls for checking the combination of power, speed, pulse frequency, and power curve. If one side cuts through while the other develops dross, or an opening in a round tube is skewed, check whether the beam and nozzle centers coincide. These symptoms require different checks; one parameter cannot resolve every edge defect.
The first part verifies the program, material, workholding, and process condition. In-process sampling and last-part inspection still serve their own purposes after the first part passes. A single acceptable sample demonstrates conformity only under its corresponding conditions; it does not establish the stability of the entire subsequent batch.
Which tasks still require people after automatic cutting begins
Automatic cutting, loading, and sorting are separate functions. Replenishing stock, changing bins, clearing dross, maintenance, and troubleshooting may still require people. Automated equipment also requires monitoring and exception handling. Training should cover programs, materials, automatic mechanisms, recovery from abnormal conditions, daily checks, and safe operation, rather than only the cutting interface.
Production and maintenance also require different handling. Before entering the machine for maintenance, activate the emergency stop, shut the machine down, disconnect the main power, and confirm that it is fully de-energized. Guards, interlocks, extraction, and controlled access are also operating conditions. A laser classification label cannot replace risk controls for the complete machine.
Before moving from trial cutting to continuous production, confirm one final point: with the current program, clamping, and process settings, do the cut edges and dimensions meet this part's requirements?